
What is pharmaceutical supply chain management?

Pharmaceutical supply chain management is an essential part of the healthcare industry because it ensures that medicines, vaccines, and other medical products reach patients safely and on time. From manufacturing pharmaceutical products to delivering them to hospitals, pharmacies, and healthcare facilities, every step requires careful planning, monitoring, and coordination. 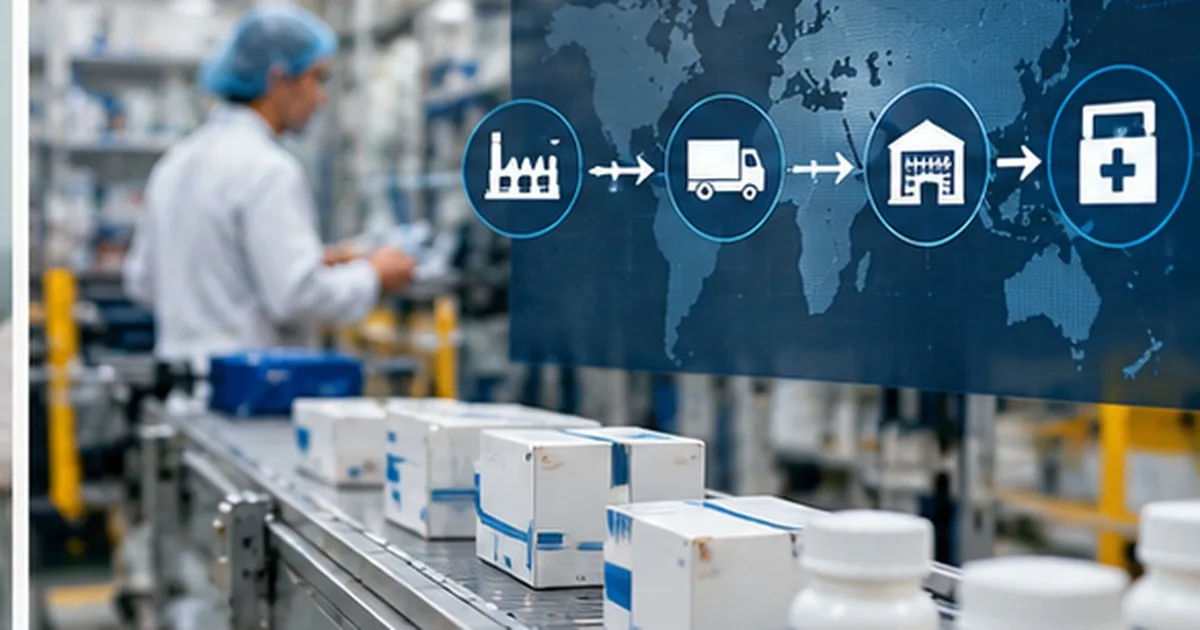 An efficient system helps protect medicine quality, reduce waste, control costs, and support better patient care.
To understand what is pharmaceutical supply chain management, it is important to look at how medicines move through different stages, including sourcing raw materials, manufacturing, packaging, storage, transportation, and final distribution. Unlike ordinary consumer goods, pharmaceutical products often require strict temperature control, accurate documentation, and compliance with health regulations. Even a small mistake can affect product quality or delay essential treatment.
In today's healthcare environment, pharmaceutical supply chain management has become more important than ever. Growing demand for medicines, international trade, changing regulations, and unexpected disruptions make the process increasingly complex. Businesses must use reliable systems and effective strategies to maintain a steady supply of safe and effective medicines.
This comprehensive guide explains how pharmaceutical supply chain management works, its major components, benefits, challenges, and the technologies that are transforming the industry.
Pharmaceutical Supply Chain Management
Pharmaceutical supply chain management refers to the planning, coordination, and control of activities involved in producing and delivering medicines. It connects suppliers, manufacturers, distributors, logistics providers, pharmacies, hospitals, and other healthcare organizations.
The main objective is to make the right medicine available in the right quantity, at the right location, and at the right time. Products must also remain safe, effective, and compliant with applicable quality standards throughout their journey.
Pharmaceutical supply chain management differs from the management of many other products because medicines directly affect human health. Some products expire quickly, while others require refrigeration or protection from light, moisture, and contamination.
For example, vaccines may require a carefully controlled temperature throughout transportation and storage. If the required conditions are not maintained, their quality may be compromised even when the packaging appears undamaged.
An effective supply chain therefore combines logistics, inventory management, quality assurance, regulatory compliance, and information sharing.
How Does the Pharmaceutical Supply Chain Work?
The pharmaceutical supply chain consists of several connected stages. Each stage contributes to ensuring that medical products are available and suitable for patient use.
1. Raw Material Sourcing
The process begins with obtaining the materials required to manufacture medicines. These may include active pharmaceutical ingredients, chemical compounds, excipients, packaging materials, and other production supplies.
Active pharmaceutical ingredients are the substances responsible for producing a medicine's intended therapeutic effect. Excipients are additional ingredients that help give a medicine its form, stability, taste, or delivery characteristics.
Pharmaceutical companies must work with qualified suppliers who meet established quality requirements. They may inspect facilities, review documentation, test incoming materials, and assess supplier performance before approving purchases.
Reliable sourcing reduces the risk of contamination, production delays, and inconsistent product quality.
2. Pharmaceutical Manufacturing
Once raw materials have been approved, they move into the manufacturing process. Depending on the product, production may involve mixing, chemical processing, formulation, tablet compression, sterilization, filling, or other specialized operations.
Manufacturers must follow appropriate production standards, including Good Manufacturing Practices (GMP). These standards help ensure that products are consistently produced and controlled according to their intended quality.
Production planning is also important. Companies must estimate demand, schedule manufacturing activities, allocate resources, and maintain sufficient materials to meet expected orders.
Poor planning can result in shortages, excess inventory, or production interruptions.
3. Quality Control and Product Release
Before medicines can be distributed, manufacturers must complete the required quality checks and release procedures.
Depending on the product, testing may evaluate identity, strength, purity, stability, sterility, and other specifications. Packaging and labeling must also meet relevant requirements.
Products that fail established quality criteria must not be released for routine distribution. Investigations may be necessary to identify the cause and determine appropriate corrective action.
Quality control is particularly important because defective or improperly manufactured medicines can create serious risks for patients.
4. Packaging and Labeling
After production and the relevant quality checks, medicines are packaged to protect them during storage and transportation.
Packaging may include bottles, blister packs, cartons, sealed containers, or specialized temperature-controlled materials. Labels provide important information such as dosage strength, batch number, expiration date, storage conditions, and other required details.
Accurate labeling supports safe use and helps distributors identify products throughout the supply chain.
Errors in labeling, packaging, or batch identification can cause confusion, regulatory problems, and potentially dangerous medication mistakes.
5. Warehousing and Storage
Pharmaceutical products are stored in warehouses, distribution centers, and specialized facilities before reaching customers.
Storage conditions must match each product's requirements. Some medicines can be kept at controlled room temperature, while others require refrigeration or frozen storage.
Warehouses also need effective inventory systems to track product quantities, locations, batch numbers, and expiration dates.
Many organizations use the first-expiry-first-out method, which prioritizes distributing products with the earliest expiration dates, provided they remain suitable for use and meet customer requirements.
Proper storage helps reduce damage, prevent unnecessary waste, and maintain medicine quality.
6. Transportation and Distribution
The next stage involves moving pharmaceutical products from manufacturers or warehouses to distributors, hospitals, pharmacies, clinics, and other authorized destinations.
Transportation methods may include road, air, rail, or sea freight. The appropriate option depends on delivery deadlines, product characteristics, distance, cost, and infrastructure.
Some products require validated packaging, temperature monitoring, security measures, or specialized vehicles. Logistics providers must follow applicable distribution requirements and maintain the necessary records.
Reliable transportation helps ensure that essential medicines arrive in good condition and are available when patients need them.
7. Delivery to Healthcare Providers and Patients
The final distribution stage connects pharmaceutical products with the organizations and people who need them.
Hospitals use inventory systems to maintain supplies for wards, pharmacies dispense prescribed medicines, and clinics manage products used during treatment.
In some healthcare systems, approved home-delivery services also provide medicines directly to patients.
Accurate order processing, safe handling, and timely delivery are critical at this stage. Effective communication between suppliers and healthcare providers helps prevent shortages and supports continuity of care.
What Are the Main Components of Pharmaceutical Supply Chain Management?
Understanding what is pharmaceutical supply chain management also requires examining the activities that keep the entire system operating efficiently.
Demand Forecasting and Planning
Demand forecasting estimates how many medicines will be required over a particular period. Organizations may consider historical sales, prescription patterns, seasonal illnesses, population needs, and public health programs.
For example, demand for certain respiratory medicines may increase during particular seasons. Forecasting helps manufacturers and distributors prepare suitable inventory before demand rises.
Accurate forecasts reduce the risk of both shortages and overstocking. However, unexpected outbreaks and sudden changes in prescribing practices can make predictions difficult.
Inventory Management
Inventory management involves monitoring available stock and determining when products should be reordered.
Pharmaceutical organizations must balance product availability with storage costs, expiration risks, and changing demand.
Excess inventory ties up capital and increases the possibility of expired medicines. Insufficient inventory can delay treatment and force healthcare providers to seek alternative products.
Effective inventory systems use stock records, reorder points, expiration tracking, and demand information to support better decisions.
Supplier Relationship Management
Pharmaceutical companies often depend on several suppliers for ingredients, packaging, equipment, and specialized services.
Supplier relationship management involves evaluating reliability, quality, delivery performance, financial stability, and compliance.
Working with qualified suppliers can improve communication and reduce interruptions. Depending on the product and available alternatives, companies may also qualify multiple suppliers to reduce dependence on a single source.
Quality Assurance and Regulatory Compliance
Quality assurance covers the procedures and systems designed to maintain product quality throughout the supply chain.
Organizations must follow applicable laws, licensing requirements, manufacturing standards, distribution rules, and documentation practices.
Requirements differ across countries and product categories. Companies operating internationally must understand the regulations that apply to each market.
Maintaining accurate records also helps organizations investigate problems, demonstrate compliance, and respond effectively to inspections.
Logistics and Information Management
Logistics management coordinates transportation, warehousing, packaging, and delivery schedules.
Information management connects these activities through inventory software, order systems, shipment records, and product-tracking tools.
When information is accurate and available to authorized teams, organizations can identify delays, respond to changes, and coordinate activities more efficiently.
Why Is Pharmaceutical Supply Chain Management Important?
Pharmaceutical supply chain management affects healthcare quality, business performance, and public health.
Ensures Medicine Availability
Patients depend on consistent access to medicines for both short-term illnesses and long-term conditions.
A well-managed supply chain helps healthcare facilities maintain adequate supplies and prepare for predictable changes in demand.
Better planning can also reduce emergency purchasing and help organizations respond to shortages more effectively.
Protects Medicine Quality
Medicines can be damaged by unsuitable temperatures, humidity, contamination, or poor handling.
Strong storage and distribution practices help preserve product quality throughout transportation and delivery.
Temperature monitoring, product inspections, and documented handling procedures are particularly important for sensitive medicines.
Reduces Costs and Waste
Pharmaceutical products can be expensive to manufacture, store, transport, and replace.
Effective planning reduces unnecessary stock, inefficient transportation, expired inventory, and avoidable emergency shipments.
These improvements can help pharmaceutical companies and healthcare providers control operating costs while maintaining reliable service.
Improves Patient Safety
Accurate batch records and product-tracking systems help organizations identify affected products when a quality issue occurs.
If a medicine must be recalled, reliable records can help determine which batches were distributed and where they were sent.
This allows companies and healthcare organizations to respond more quickly and reduce the risk of affected products reaching patients.
Supports Public Health Programs
Vaccination campaigns, emergency medical services, and disease-control programs often depend on coordinated pharmaceutical distribution.
Reliable supply chains help ensure that essential products reach the appropriate locations, including areas with limited healthcare infrastructure.
Major Challenges in Pharmaceutical Supply Chain Management
Despite its importance, pharmaceutical supply chain management faces several significant challenges.
Temperature Control and Cold Chain Management
Certain medicines, vaccines, and biological products require strict temperature control. This specialized process is known as cold chain management.
Temperature problems can occur during storage, transportation, loading, unloading, or temporary transfers between facilities.
Organizations can reduce these risks by using suitable packaging, calibrated monitoring equipment, qualified transport providers, and documented procedures for temperature excursions.
Global Supplier Dependence
Many pharmaceutical products rely on ingredients or materials sourced from multiple countries.
International sourcing can offer cost advantages, but it may also expose organizations to shipping delays, geopolitical tensions, trade restrictions, natural disasters, and supplier shutdowns.
Companies can manage these risks by assessing supplier concentration, qualifying alternatives where practical, and developing contingency plans for critical products.
Counterfeit and Illegitimate Medicines
Counterfeit or illegally distributed medicines can enter poorly controlled supply networks and pose serious health risks.
Packaging checks, supplier verification, product serialization where required, secure distribution channels, and traceability systems help reduce these risks.
Healthcare providers should purchase medicines through authorized suppliers and follow established procedures for reporting suspicious products.
Regulatory Complexity
Different markets may have different requirements for product registration, labeling, serialization, importation, storage, and distribution.
Organizations must keep their procedures current and ensure that employees understand the rules relevant to their responsibilities.
Failure to meet applicable requirements can lead to shipment delays, product holds, financial penalties, or other consequences.
Demand Uncertainty and Medicine Shortages
Unexpected disease outbreaks, manufacturing problems, and sudden increases in demand can create shortages.
Some medicines also have limited suppliers or complex production requirements, making rapid replacement difficult.
Demand monitoring, appropriate safety stock, early risk detection, and coordinated communication can help reduce the impact of disruptions.
Data and Cybersecurity Risks
Modern supply chains rely on digital platforms to manage orders, inventory, shipment information, and product records.
System outages, inaccurate data, unauthorized access, or cyberattacks can interrupt operations.
Organizations should protect systems through access controls, backups, security monitoring, employee training, and tested recovery procedures.
How Technology Is Transforming Pharmaceutical Supply Chains
Technology helps pharmaceutical organizations improve visibility, planning, and control.
Artificial Intelligence and Predictive Analytics
Artificial intelligence can analyze historical demand, sales patterns, supplier performance, and other operational data.
These tools may help identify potential shortages, predict demand changes, and improve inventory planning.
However, predictions depend on data quality and appropriate model design. Human oversight remains important, especially when decisions affect medicine availability or patient safety.
Internet of Things and Temperature Monitoring
Internet of Things devices can collect information from sensors installed in storage facilities, transport vehicles, and shipping containers.
Temperature sensors can alert staff when readings move outside specified limits. Location tracking can also improve shipment visibility.
These tools support faster intervention, although alerts must be linked to clear procedures and responsible personnel.
Blockchain and Traceability
Blockchain is a type of distributed digital record system that can support shared tracking information among participating organizations.
In pharmaceutical distribution, it may help improve the visibility of product movements and recorded transactions.
However, blockchain does not automatically guarantee that a product is genuine or that information entered into the system is accurate. Its value depends on implementation, data quality, governance, and cooperation among participants.
Enterprise Resource Planning Systems
Enterprise resource planning systems connect functions such as purchasing, manufacturing, inventory, finance, and order management.
By integrating information, these platforms help organizations reduce duplicated records and coordinate activities across departments.
They can also provide managers with reports that support operational planning and performance monitoring.
Automated Warehousing
Automated storage systems, barcode scanners, robotics, and warehouse management software can improve picking accuracy and inventory visibility.
Automation may reduce repetitive work and help facilities process large volumes of orders.
Nevertheless, pharmaceutical warehouses still require suitable validation, maintenance, employee training, and controls to ensure that automated processes meet quality requirements.
Best Practices for Effective Pharmaceutical Supply Chain Management
Organizations can strengthen their supply chains by adopting practical, consistent management strategies.
Establish Strong Quality Procedures
Quality requirements should apply to suppliers, manufacturing facilities, warehouses, transport providers, and distribution partners.
Written procedures, staff training, documented inspections, and corrective actions help maintain consistent standards.
Companies should also investigate recurring problems rather than treating every incident as an isolated event.
Improve Supply Chain Visibility
Managers need reliable information about inventory, purchase orders, production schedules, and shipments.
Integrated systems and regular communication can help identify problems before they affect customers.
Organizations should define which information must be shared, who can access it, and how discrepancies will be resolved.
Develop Risk Management Plans
Risk assessments should identify vulnerable suppliers, critical products, transportation routes, and facilities.
Organizations can then establish backup arrangements, alternative shipping plans, appropriate safety stock, and escalation procedures.
Plans should be reviewed periodically and tested through realistic scenarios.
Monitor Key Performance Indicators
Key performance indicators, or KPIs, help managers evaluate supply chain performance.
Useful measures include:
-
Order fulfillment rate: The proportion of orders delivered as requested.
-
On-time delivery rate: The percentage of shipments arriving within the agreed timeframe.
-
Inventory accuracy: How closely recorded stock matches actual stock.
-
Product waste rate: The proportion of inventory lost through expiration or damage.
-
Temperature excursion rate: The frequency of temperature deviations in controlled shipments.
-
Supplier performance: How consistently suppliers meet agreed quality and delivery requirements.
KPIs should be interpreted together rather than in isolation. For example, reducing inventory costs is not a successful improvement if it causes frequent medicine shortages.
Strengthen Staff Training
Employees must understand proper handling, storage, documentation, hygiene, security, and escalation procedures.
Training should reflect each employee's responsibilities and be updated when processes or regulations change.
Well-trained staff are better prepared to recognize unusual conditions and report potential problems promptly.
The Role of Pharmaceutical Supply Chain Management in Pakistan
Pharmaceutical supply chain management is especially relevant in Pakistan, where medicine availability depends on coordination among manufacturers, importers, distributors, hospitals, pharmacies, and regulatory authorities.
Organizations must manage transportation challenges, changing demand, storage requirements, supplier reliability, and compliance with applicable national regulations.
Maintaining reliable access to medicines can be particularly challenging when products depend on imported ingredients or specialized manufacturing materials.
Better inventory visibility, qualified suppliers, appropriate storage facilities, and accurate product records can help organizations improve efficiency.
Hospitals and pharmacies can also benefit from regular stock reviews, expiration monitoring, demand planning, and communication with authorized distributors.
Digital systems may further support distribution planning and product traceability, provided they are implemented with suitable security and quality controls.
For pharmaceutical businesses in Pakistan, the objective should not simply be to reduce costs. It should be to maintain product quality, comply with applicable requirements, and ensure that patients can access the medicines they need.
Conclusion
Pharmaceutical supply chain management is the coordinated process of sourcing, manufacturing, storing, transporting, and distributing medicines while maintaining their quality, safety, and availability. It connects suppliers, pharmaceutical manufacturers, logistics providers, distributors, hospitals, pharmacies, and patients through a network of activities that must work together reliably.
Understanding what is pharmaceutical supply chain management helps explain why every stage matters. Careful sourcing protects the quality of raw materials, controlled manufacturing ensures consistent production, effective warehousing preserves products, and reliable transportation supports timely delivery. Inventory planning and accurate documentation further reduce shortages, waste, and operational risks.
Although pharmaceutical supply chains face challenges such as temperature control, supplier dependence, regulatory complexity, counterfeit medicines, and unpredictable demand, organizations can address many of these issues through better planning and risk management. Technologies such as artificial intelligence, connected sensors, integrated business software, and traceability systems can provide additional support when implemented responsibly.
Ultimately, an effective pharmaceutical supply chain is not measured only by delivery speed or financial savings. Its real value lies in ensuring that safe, effective, and properly handled medicines reach the people who depend on them. By combining strong quality standards, reliable partnerships, skilled employees, and continuous improvement, pharmaceutical organizations can build supply chains that support both business performance and better healthcare outcomes.